If you’re a manufacturer, construction crew lead, or product designer, you know that even the smallest parts make the biggest difference in holding everything together. As a supplier of auxiliary fastening parts, I’ve seen firsthand how a misstep in installation can turn a solid assembly into a safety hazard or a costly rework. That’s why I’m breaking down the clear, step-by-step process we share with every client to make sure our fasteners do what they’re designed to do—no shortcuts, no guesswork. Auxiliary Fastening Parts

First, let’s start with pre-installation prep, because skipping this step is where most problems begin. A lot of people grab a part, a tool, and dive in, but that’s a mistake. Auxiliary fastening parts range from clips and brackets to threaded inserts, rivet nuts, and self-clinching nuts—each built for a specific material: wood, metal, plastic, or composite. Before you even pick up a tool, you need to do two checks: material compatibility and part verification. I always advise clients to match our parts to their base material, not just their application. For example, a self-clinching steel fastener won’t hold up in a soft aluminum panel, and a plastic push clip won’t secure heavy HVAC ductwork. We include a material spec sheet with every order, but it’s worth cross-referencing with your assembly’s load requirements. If you’re working with high-vibration parts—think automotive interiors or industrial machinery—opt for a locking auxiliary fastener (like a nylon insert nut or a spring clip) instead of a standard one to prevent loosening over time.
Next, verify your part’s dimensions. It sounds obvious, but I’ve had more than one client call us panicking because they ordered a ¼-inch rivet nut and tried to install it in a ⅜-inch hole. Auxiliary fasteners rely on tight tolerances, so a wrong size means either the part won’t fit or it will move and fail. Take 30 seconds to measure the hole in your base material against the fastener’s diameter and length. Also, check for damage: even a tiny burr on a rivet or a bent tab on a bracket can throw off alignment. We package our parts in protective plastic trays, but if yours arrived loose or scuffed, set those aside and grab a new set. It’s not worth risking a full assembly over a $0.10 fastener.
Once you’ve confirmed you have the right parts, move to hole preparation. This step often gets overlooked, but it’s make-or-break. A clean, properly sized hole ensures the fastener seats correctly and distributes load evenly. For metal panels, use a drill bit matched to your fastener’s recommended hole size—we list this on each part’s packaging and in our product guide. If you’re working with wood or composite, a stepped drill bit works well because it cuts a smooth hole without splintering the material’s backside. I’ve seen crews skip hole deburring too: a sharp metal edge around the hole can cut through a plastic fastener’s sleeve or scratch a threaded insert’s threads, leading to stripped fasteners later. Use a deburring tool or a small file to smooth the hole’s edges, and blow away all debris with compressed air before moving on—shavings or dust trapped behind the fastener can keep it from seating flush.
Now, let’s get to installing, and I’ll break this down by the most common auxiliary fastening parts our clients use, since installation varies by type. First, self-clinching nuts and standoffs—super popular in electronics enclosures and sheet metal assemblies. For these, align the fastener so the clinching tabs (the small projections along the part’s edge) sit inside the hole. Once aligned, use a rivet press or a manual punch tool to apply steady, even force until the fastener’s flange sits flush with the sheet metal. Don’t use a hammer here—striking too hard can bend the flange or crack thin metal. For thin gauge materials (under 0.04 inches), we recommend a soft metal backing plate to distribute the press force, so the fastener doesn’t deform. After installation, test it by turning a screw into the threaded hole—if it spins freely and doesn’t wobble, you’re good to go. If it doesn’t turn, you’ve either misaligned the fastener or left debris in the hole, so remove it and start over.
Next, push-in clips and retention fasteners, used a lot in automotive, furniture, and appliance assembly. These are the easiest, but they’re also easy to install incorrectly. Start by inserting the clip’s center pin into the pre-drilled hole, then push the outer flange until it clicks into place. A lot of people press too hard on the flange, which can bend the retention tabs and make the clip fall out later. Instead, feel for that distinct click—if you don’t hear it, pull slightly and reposition the clip, because the retention tabs aren’t seated properly. For parts that need to withstand vibration (like door panels), give the clip a gentle tug after installation to confirm it’s secure. If it comes loose, you either used the wrong size clip or the hole is too big, so swap it for a larger clip or add a small amount of thread-locking compound (for metal holes) to the retention tabs.
Rivet nuts (also called blind rivet nuts) are another workhorse, used when you can’t access the backside of a panel—think attaching brackets to a wall or a car’s outer frame. For these, insert the rivet nut into the hole from the front, then attach a rivet nut tool (handheld or pneumatic) to the nut’s threaded end. Squeeze the tool’s handle steadily, and the rivet nut’s body will expand, clamping tightly to the backside of the panel. Stop squeezing once the tool’s torque clicks—over-tightening will crack the panel or deform the rivet nut, and under-tightening will let it spin. After installation, test the thread by threading a bolt onto the rivet nut—if it doesn’t cross-thread and sits flush, it’s installed correctly. If the bolt is loose or the nut spins, you either didn’t expand the nut enough or the hole was too big, so try a thicker grip range rivet nut next time.
Now, the step I almost forgot to mention: post-installation inspection. This is the part that separates a good installation from a great one, and it’s non-negotiable. We tell all our clients to do a quick check after installing every auxiliary fastener. For threaded parts, test the thread engagement: make sure a screw or bolt turns smoothly without resistance (unless you’re using a locking fastener, in which case it should have slight friction to prevent loosening). For clips and rivets, tug gently to confirm they don’t move. If you’re working on a structural assembly (like a load-bearing bracket), apply a small test load—for example, tap a bracket lightly to make sure it doesn’t shift, or hold a heavy object against it to test stability. This inspection takes 10 seconds per part, but it can save you hours of repairs down the line.
Wait, I should also talk about common mistakes to avoid, since I see these every week. First, using the wrong tool for the job. A lot of people use a cordless drill to install self-clinching parts, which is too powerful and can bend the fastener. We always recommend a manual press or a pneumatic rivet tool for controlled force. Second, skipping thread locking or anti-vibration measures. Even the best auxiliary fasteners will loosen over time if they’re subject to constant movement. For exposed fasteners, add a small dab of anaerobic thread locker (low strength for easy disassembly, high strength for structural parts) to the fastener’s threads. For high-vibration applications, use locking fasteners instead of standard ones—they’re designed with nylon inserts or spring tabs that grip the threads tightly. Third, forcing a fastener into a hole. If a part won’t fit, don’t hammer it in—you’ll damage both the fastener and the base material. Double-check your dimensions, and if it still doesn’t fit, reach out to your supplier for help. We often help clients troubleshoot fit issues, because we’d rather see a part work than have it returned.
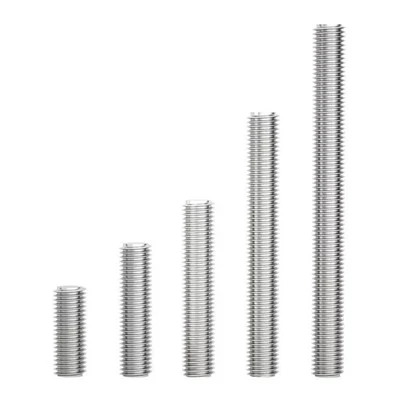
As an auxiliary fastening parts supplier, our job isn’t just to ship parts—it’s to make sure they’re installed correctly so your assemblies work as intended. If you’re working on a project and need fasteners for a specific application, or if you have questions about installation best practices, we’re here to help. Whether you’re a small workshop or a large manufacturing operation, we can provide custom fasteners tailored to your material, load, and assembly needs. Don’t leave your project’s integrity to guesswork—reach out to our team to discuss your requirements and get the right parts for the job. We’re ready to walk through your project, answer any questions you have, and supply auxiliary fastening parts that hold up to even the toughest conditions.
Auxiliary Fastening Parts References
- Bralla, J. G. (1999). Design for Manufacturability Handbook. McGraw-Hill.
- Automotive Industry Action Group (AIAG). (2021). Fastening and Joining Best Practices Manual. AIAG.
- Smith, P. F. (2018). Fastener Technology: Principles and Applications. ASM International.
- Manufacturer’s Standardization Society (MSS). (2020). Specifications for Auxiliary Fastening Components. MSS.
- International Organization for Standardization (ISO). (2019). ISO 10888: Fasteners for Structural Applications – Installation Guidelines. ISO.
Handan Hengmai Fasteners Manufacturing Co., Ltd.
Handan Hengmai Fasteners Manufacturing Co., Ltd. is one of the most professional auxiliary fastening parts manufacturers and suppliers in China. With abundant experience, we are committed to providing customized fasteners made in China with competitive price. We warmly welcome you to buy bulk high quality auxiliary fastening parts for sale here from our factory.
Address: Industrial Zone, West of Beiduanzhuang Village, Linmingguan Town, Yongnian District, Handan City, Hebei Province
E-mail: hmfasteners.cn@gmail.com
WebSite: https://www.hmfasteners.com/
