Hey everyone, if you’ve ever driven past a construction site, noticed a shiny soda can in the grocery store, or even admired a sleek gutter on a house, you’ve probably interacted with aluminum coil without even realizing it. I’ve been in the aluminum coil game for over a decade now—running our small, reliable supply operation that works with everyone from big construction companies to custom fabricators—and one question I get asked constantly is: how the heck do we turn raw bauxite into that smooth, rollable coil that’s the backbone of so many industries? Today, I’m breaking down the whole process, no stuffy jargon, just real talk from someone who’s stood in our mill watching this happen hundreds of times a week. Aluminum Coil
Let’s start with the basics, because a lot of folks don’t know where aluminum even comes from. Raw bauxite is the rock we mine, right? It’s crumbly, usually reddish-brown, and found in places like Australia, Guinea, and Brazil. First stop for that bauxite is a refinery, where we turn it into alumina—aka aluminum oxide, that white powdery stuff. If you think this part is easy, no way: it’s heated, mixed with caustic soda, dissolved, filtered to remove all the gunk, and then cooled to get that pure alumina powder. I’ve seen shipments of this powder roll into our facility, and it’s so fine it floats in the air like baby powder, but way more dusty. That alumina is what we actually turn into aluminum metal, and that happens in smelters.
Smelting is where the magic (and the power) really happens. We mix alumina with molten cryolite to lower its melting point, then stick it in a huge electrolytic cell—think of a giant steel box lined with carbon, with carbon rods hanging down from the top. Pass a massive electric current through that mix, and boom: molten aluminum sinks to the bottom of the cell. That’s super pure aluminum, like 99.5% or more. It’s liquid, hot enough to burn through gloves if you’re not careful, so the guys who handle this stuff wear layers of heat-resistant gear that looks like something out of a space movie. Once it’s ready, we siphon that molten aluminum into big crucibles, which we then pour into ingots—those big, rectangular bars you see stacked in yards. Each ingot is like 15 or 20 tons, and trust me, they’re heavy. You don’t want to drop one on your foot.
Now, we’re at our facility, and those aluminum ingots just showed up on the back of a semi. That’s where the fun (for us, anyway) begins for making coil. First step here is preheating the ingots, because if we tried to roll cold aluminum, it would crack like a cheap Christmas ornament. We stick the ingots in a huge furnace that heats them up to around 800-900°F, so they’re soft and malleable enough to shape. This takes a few hours, but it’s worth it—heating evenly is key, because if one side is hotter than the other, the metal will stretch unevenly and we’ll waste time and material.
Next up is hot rolling. This is the first time we actually shape the aluminum into a thin sheet, which will eventually become coil. We take the preheated ingot and feed it through a series of heavy-duty rolling mills—like big, thick steel rollers that squeeze the metal over and over. Each pass makes the sheet thinner and longer, kind of like rolling out pizza dough, but way heavier and way more precise. At this stage, we’re going from that big, thick ingot (like 2 feet thick) to a sheet that’s maybe a quarter-inch thick. The whole time, we spray water on the rollers and the metal to keep it cool—too much heat and the aluminum will get sticky, too little and we’ll warp it. We have guys monitoring the thickness every single second with sensors, because even a tiny variation means the whole batch is off.
Once we’ve got that hot rolled sheet, it’s time for cold rolling. Wait, why “cold” if we just heated it? Because now we’re rolling it at room temperature, which makes the aluminum stronger and gives it that smooth, shiny finish we all know. Cold rolling is where the precision really kicks in. The mills here have tiny adjustments—we can change the thickness by a fraction of a millimeter, like, seriously. If we’re making coil for soda cans, we need it super thin but still strong enough not to crumple. For gutter coil, we need it a little thicker to hold up in rain and snow. So depending on what the customer orders, we run the sheet through 5, 10, even 15 sets of cold rollers. Each pass squeezes it thinner, and we clean the metal between passes to get rid of any dirt or tiny metal shavings that would scratch the surface. This is where a lot of small suppliers mess up—they skip the extra cleaning passes, and the coil ends up with little marks that make it useless for their customers. We never cut corners here.
After cold rolling, we’ve got a long, thin aluminum sheet, but it’s not quite coil yet—we need to cut it to the right width and give it whatever finish the customer wants. First, we run it through a slitter. That’s a machine with sharp, rotating blades that cut the big, wide sheet into multiple narrower strips, exactly the width the customer ordered. I can’t tell you how many times a customer has come to us saying “we need coil for our roof panels, 12 inches wide” and we have to cut it perfectly to that, no more no less. A quarter-inch off and their panels won’t line up.
Now, the finish. This is where we tailor the coil to what it’s going to be used for. Some customers want bare aluminum—plain, shiny, used for things like electrical wiring or industrial parts. But most want a coated finish, because aluminum can rust (even though it’s called “weatherproof,” it’s not invincible to salt or moisture over time). We do a few types of coating here: there’s prepainted, where we run the coil through a coating line that sprays on a layer of paint (or sometimes a powder coat that’s baked on, which is way more durable), then cure it in an oven to make it stick. There’s also anodized coating, which is a electrochemical process that thickens the aluminum’s natural oxide layer, giving it a matte or glossy finish that’s super scratch-resistant. And for customers who need specific colors, we can mix the paint to match almost any shade—last year we did a custom forest green coil for a ski resort’s new lodges, and the color matched their brand exactly.
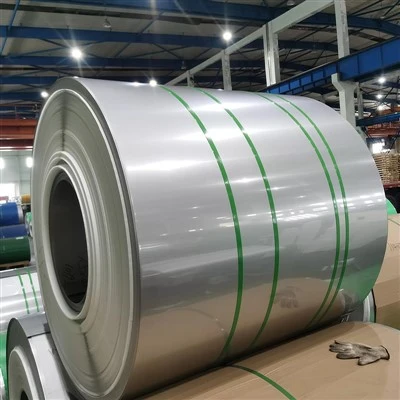
Once it’s finished, it’s time to wind it into a coil, obviously. We have huge winding machines that grab the narrow strips of coated or bare aluminum and wind them tightly onto a steel core. The tension here is important—too loose and the coils will sag or get damaged when we ship them; too tight and they’ll crease, which makes them worthless. We test every coil for tension multiple times, because if a coil is wound wrong, it can unravel during shipping and take out half a warehouse. Then we slap on labels with the alloy grade, thickness, width, and finish, and get it ready for delivery.
Wait, I should mention quality control, because this is non-negotiable for us. Every step of the process has a check: we test the purity of the aluminum when it comes in, check the thickness every 10 feet during rolling, run the coating through a scratch test and a weather resistance test, and even unroll a random coil at the end to make sure there are no hidden marks. Last quarter we had a batch where the coating was too thin, so we pulled it all back and re-did it—even though that cost us a few thousand bucks, we’d rather lose money than a customer, because word travels fast in this industry.
At the end of the day, aluminum coil is way more than just shiny metal. It’s ingots from a smelter, rolled thousands of times, coated to last, and tailored to fit exactly what someone needs. Whether you’re a roofer needing durable coil for a new building, a fabricator making custom kitchen appliances, or a manufacturer of automotive parts, getting the right coil makes or breaks your project.
If you’re in the market for aluminum coil—whether it’s bare, prepainted, anodized, any alloy or thickness—we work with businesses of all sizes, from small local contractors to large national construction firms. We offer custom orders, fast turnaround, and we stand behind every coil that leaves our facility. Don’t hesitate to reach out to us to chat through your needs, get a quote, or ask any questions about the process—we’re always happy to help.
Galvanized Steel References:
- Aluminum Association. (2022). Aluminum Production: From Bauxite to Finished Product.
- International Institute of Aluminum. (2021). Rolling and Processing of Aluminum Coil.
- U.S. Energy Information Administration. (2020). Energy Use in Aluminum Smelting and Processing.
Wuxi Jin Ming Jian De Industry & Trade Co., Ltd.
Wuxi Jin Ming Jian De Industry & Trade Co., Ltd. is one of the most professional aluminum coil manufacturers and suppliers in China, also supports customized service. With abundant experience, we warmly welcome you to wholesale CE approved aluminum coil in stock here from our factory. If you have any enquiry about quotation, please feel free to email us.
Address: 2102-2105, Yuexing Building, Guangnan Road, Liangxi District, Wuxi City, Jiangsu Province, China.
E-mail: info@wxjmjdss.com
WebSite: https://www.jmjdsteelexp.com/
